


Stainless Steel CNC Machining
Stainless steel CNC machining is rarely a matter of choosing “stainless” and sending a model. Grade, product form, condition, heat treatment, corrosion exposure, welding, surface requirements, and documentation all affect the order. Machining also brings practical risks: work hardening, heat concentration, tool wear, burrs, thin-wall movement, and contamination during handling or finishing. A complete RFQ should make these variables visible before price, timing, and inspection scope are agreed.
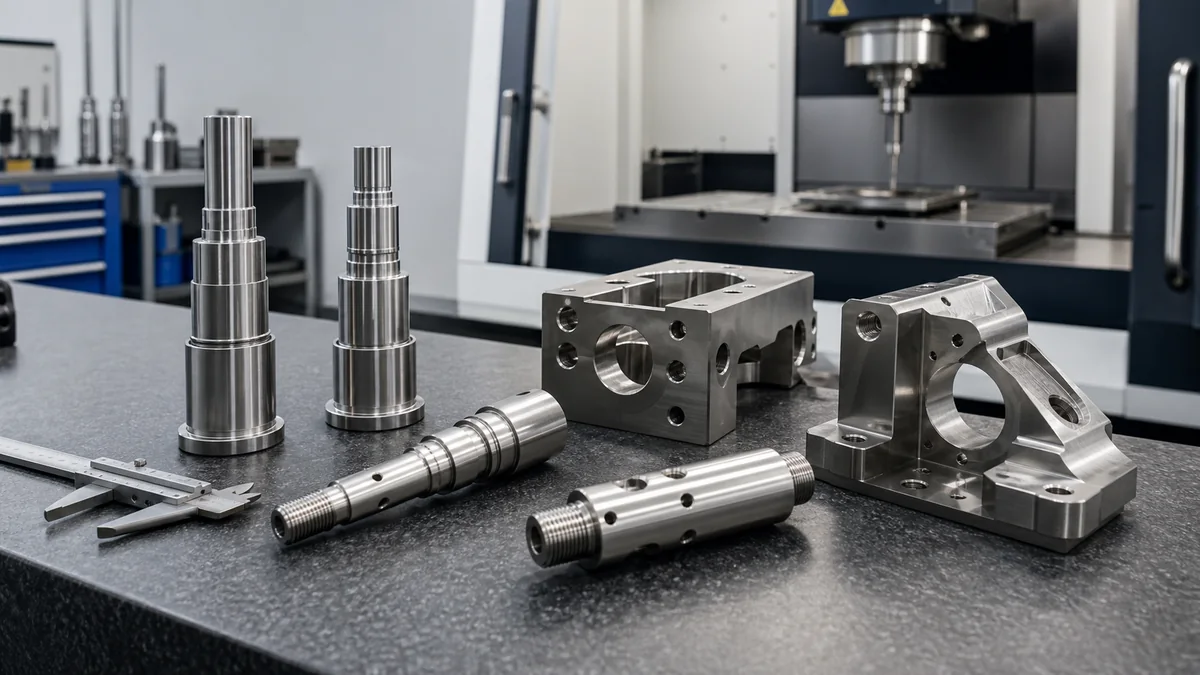
Process fit
Select the route from part geometry and function.
Quality planning
Connect critical features to an inspection plan.
Project review
Review drawings and requirements before quotation.
Buy the grade, condition, and product form
Stainless grades are not interchangeable. The same family may include low-carbon versions, free-machining variants, precipitation-hardening grades, and different supplied conditions. Specify the full designation and any governing material specification. If alternatives are acceptable, list them or require written approval before substitution.
| Common selection | Why buyers consider it | What to clarify |
|---|---|---|
| 304 or 304L | General corrosion resistance, availability, fabrication, and broad use | Exact grade, low-carbon need, product form, finish, and exposure |
| 316 or 316L | Considered where service conditions need a different corrosion response | Media, temperature, cleaning chemicals, grade, and acceptance standard |
| 17-4 PH | Considered when a precipitation-hardening stainless grade fits the design | Required condition, heat-treatment responsibility, properties, and inspection stage |
| 303 | Often evaluated for machinability in suitable environments | Corrosion, welding, regulatory, and application limits |
| Specialty grades | Used when service conditions justify a specific material | Specification, condition, sourcing, processing, testing, and documentation |
A grade name may not define bar, plate, casting, or forged stock, nor the supplied surface and mechanical condition. These differences can affect machining, distortion, traceability, and performance. State whether mill documentation, heat or lot traceability, or independent testing is required before material is purchased.
Work hardening and heat change the machining plan
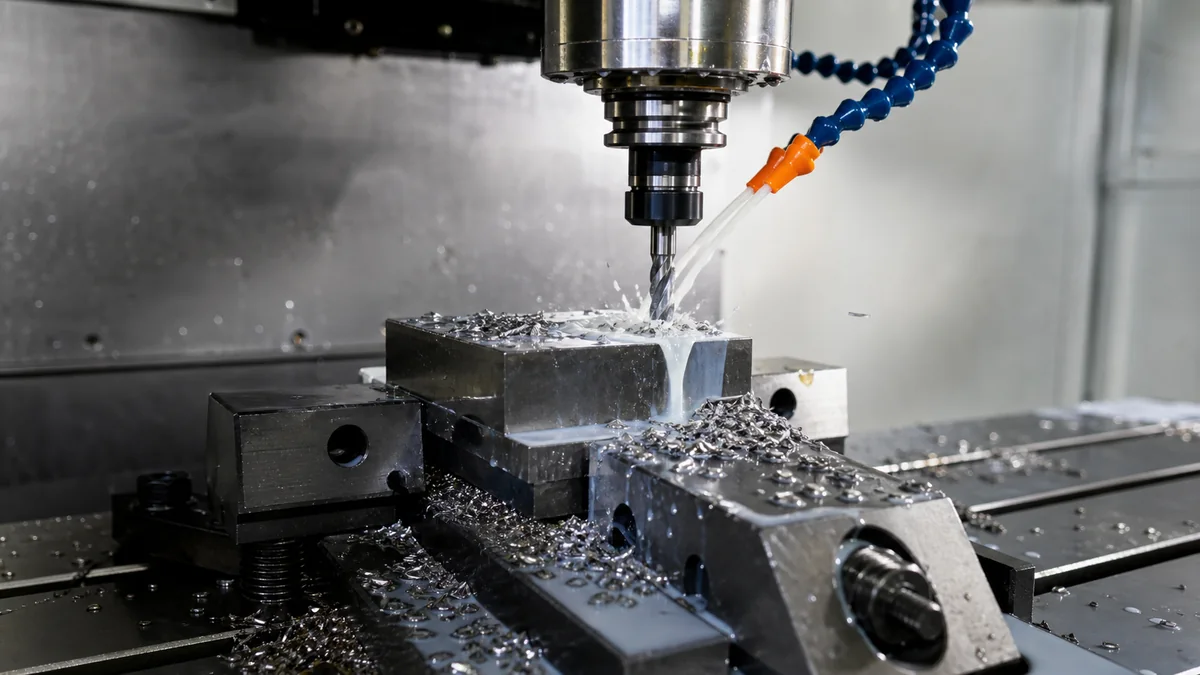
Many stainless steels can harden at the cut when a tool rubs instead of removing a controlled chip. Heat also tends to remain near the cutting zone, which can accelerate tool wear and affect the surface. The response depends on grade, condition, geometry, tool access, setup stability, coolant strategy, and required finish.
Buyers do not need to prescribe cutting parameters, but should avoid inaccessible features or repeated light finishing requirements without a functional reason. Deep narrow slots, small radii, interrupted cuts, long-reach tools, and difficult deburring can raise risk. A supplier may use rigid setups, suitable tool geometry, controlled engagement, effective chip evacuation, and planned tool replacement. These are process decisions, not universal guarantees.
For milling, turning, and related routes, see our CNC machining services.
Control burrs at edges, threads, and passages
Burr requirements should identify where raised or loose material creates risk. Stainless burrs can persist around holes, intersecting passages, slots, threads, and thin edges. “Deburr all edges” does not explain whether an edge must remain sharp, receive a controlled break, seal against another part, or meet a cosmetic requirement.
- Mark fluid, vacuum, pneumatic, and cleaning passages where debris is unacceptable.
- Identify sealing edges, O-ring grooves, valve seats, and gasket faces.
- State whether thread starts need a lead-in and how cleanliness is assessed.
- Define edge breaks only where size matters to fit, handling, or fatigue behavior.
- Show cosmetic faces where hand-finishing marks are restricted.
- Agree how inaccessible cross-holes and internal intersections are inspected and cleaned.
Edge finishing can change nearby dimensions and texture. Call out functional lands, sharp interfaces, and thin lips rather than relying on a general note.
Specify passivation and surface condition clearly
Passivation is not a generic synonym for cleaning or polishing. Identify the required process or governing specification, applicable surfaces, pretreatment, post-process testing or documentation, and responsible party. The requirement depends on alloy, service environment, prior machining, handling, and the buyer’s quality system.
Parts may require an as-machined finish, directional brushing, bead blasting, polishing, electropolishing, coating, or a combination. Each can affect appearance, edge definition, texture, dimensions, cleanliness, and inspection. Define visible faces, grain direction where relevant, acceptable variation, and areas that must not be altered. See our Dienstleistungen der Oberflächenveredelung; exact availability and acceptance criteria must be confirmed per order.
If unintended iron contamination is a risk, state required separation, cleaning, verification, and evidence instead of assuming normal shop practice matches the application.
Design thin walls for machining and inspection
Thin stainless features can move during clamping, cutting, heating, and release. Uneven stock removal may redistribute residual stress. Risk is higher for tall walls, broad plates, slender rings, asymmetric pockets, and tight flatness or profile requirements.
If function allows, increase thickness, use uniform sections, add ribs or flanges, enlarge radii, and avoid abrupt transitions. Temporary supports may be removed late. A supplier may plan balanced roughing, staged operations, lower-force finishing, custom jaws, or intermediate checks, but the route must follow the actual geometry and condition.
Define whether a flexible part is measured free-state, restrained, or assembled. Name support points, fixture force, temperature condition, and mating components if they affect acceptance. Without a shared method, the same part may produce different results on different fixtures.
Use DFM to protect drawing intent
DFM should reduce tool reach, rubbing, setups, and ambiguous inspection while preserving critical interfaces. Separate functional tolerances from dimensions inherited from the CAD model.
- Use the largest practical internal radii and avoid deep, narrow cavities without a clear need.
- Give tools and gauges access to bores, grooves, shoulders, and internal threads.
- Dimension hole patterns, sealing faces, and rotating features from functional datums.
- Avoid blanket tight tolerances; identify fits, runout, flatness, and position individually.
- Clarify blind-hole depth, usable thread depth, bottom form, and allowed relief.
- Review thin edges and interrupted features for burr removal and distortion.
- Include passivation, polishing, masking, and appearance before quotation.
- State whether heat treatment or finishing occurs before or after final inspection.
Review Your Stainless Steel Part
Send the current drawing and project requirements for review.
Build quality checks around functional risk
A dimensional report cannot prove material grade, and a material certificate cannot prove a sealing face or thread was made correctly. Connect each requested record to a failure mode.
| Risk | RFQ instruction | Evidence to agree |
|---|---|---|
| Wrong grade or condition | Name material, condition, product form, and substitution rule | Material documentation and traceability |
| Damaged functional surface | Define surface and finish requirement | Agreed visual, texture, hardness, or relevant check |
| Burrs or debris | Identify critical edges and passages | Deburring, cleaning, and inspection scope |
| Thin-part movement | Define free-state or restrained acceptance | Measurement setup and readings |
| Datum misalignment | Number critical relationships | Focused dimensional report |
| Passivation mismatch | State process, surfaces, and documentation | Processor record or acceptance check |
Confirm revision, units, projection, general tolerance, and precedence between model and drawing. Identify special gauges, mating parts, leak tests, cleanliness checks, and inspection fixtures before quotation. Define sampling or full-check expectations.
Application details change the material decision
Stainless machined parts appear in fluid handling, food and packaging equipment, laboratory instruments, medical-device development, marine hardware, automation, pumps, valves, fasteners, and exposed assemblies. The label alone is not enough to select a grade or finish.
Describe chemicals, moisture, temperature, pressure, cleaning cycles, loads, wear, welding, contact materials, and regulatory constraints. A fluid component may prioritize wetted surfaces, passages, seals, and cleanliness. An instrument part may prioritize datum stability and appearance. A welded assembly may require attention to grade variant and post-process condition.
Compare quotations on the same scope
Differences often reflect material condition, stock size, removal, tool access, setup count, burr control, finishing, inspection, documentation, and packaging—not only an hourly rate.
- Confirm grade, condition, product form, specification, and substitution approval.
- Verify passivation, polishing, blasting, masking, and cosmetic scope.
- Check when dimensions are accepted relative to heat treatment and finishing.
- List characteristics included in inspection reporting.
- Clarify cleaning, contamination control, and passage inspection.
- Separate machining, outside processing, and transportation timing.
- Specify packaging for finished, sealing, or corrosion-sensitive surfaces.
Prepare a complete stainless steel RFQ
Send a 3D model and controlled PDF drawing with matching revisions. Include quantity, grade, condition, product form, finish or passivation, critical dimensions, general tolerances, documentation, destination, and requested timing. State which file governs if they conflict.
Add service environment, mating parts, weld or heat-treatment sequence, cleanliness, cosmetic faces, edge conditions, and measurement state for flexible parts. Number characteristics requiring reports. If a standard applies, provide its exact designation and revision.
Request a stainless steel machining review
Send files and requirements through our Kontakt page. CNCMAVEN can review the supplied grade, geometry, finish, and inspection scope and raise DFM or clarification questions before an order is confirmed. State mandatory material, passivation, traceability, cleanliness, and testing requirements explicitly.
Frequently asked questions
They have different alloy chemistry and application suitability. Select from the actual corrosion environment, cleaning media, fabrication, mechanical, documentation, and regulatory requirements rather than a general ranking.
Low-carbon variants are selected when fabrication and service requirements justify them, often around welding or corrosion considerations. State the exact grade and governing specification.
Rubbing or repeated light engagement can harden material near the cut and increase heat and tool wear. Geometry, access, rigidity, chip removal, and machining strategy influence the risk.
No. The need depends on alloy, prior processing, contamination risk, service environment, customer specification, and quality requirements. Define process, scope, and evidence when mandatory.
Define whether acceptance is free-state, restrained, or assembled. Document support points, fixture conditions, temperature considerations, and critical dimensions.
Include model and drawing revision, quantity, grade, condition, product form, finish or passivation, tolerances, critical features, edge and cleanliness requirements, documentation, destination, and timing.
Request a Stainless Steel Machining Review
Send the current drawing and project requirements for review.